Who This Checklist Is For
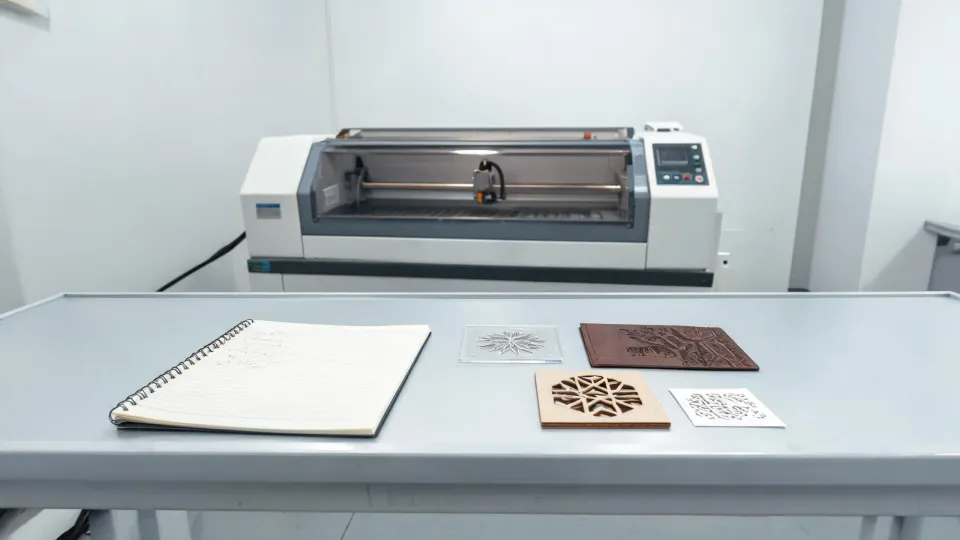
If you have a laser job that has to leave your shop in the next 24 to 48 hours, this list is for you. I coordinate production at a custom engraving shop, and we run Boss Laser equipment every day: an LS-1630 for acrylic, wood and small production parts, a Boss Laser LS-3655 for large-format sheet work, and a laser fiber marker for metal tags and components. I have triaged more than 200 rush orders in the last six years, from a $200 same-day engraving to a $15,000 production run with a two-day window.
It took me about three years and 150 orders to understand that a pre-flight check is not extra time. Skip five minutes of inspection and you can lose five hours to rework. The job that made this stick is in step 4.
Plan the Job (Steps 1-3)
Step 1: Open the Boss Laser LS 1630 manual before you touch material
Start with the Boss Laser LS 1630 manual, not with your memory of the last job that looked the same. The manual covers machine-specific setup: recommended speed and power ranges, lens requirements, focal distance, and the order of operations in the control software. That is the difference between a four-minute setup and one that burns four test pieces.
This matters even more when the deadline is tight. If the machine had a tube change or an optics swap since your last run, it will not behave the way it did last month. Keep the manual accessible. We keep a printed copy next to the control PC. Sounds like a no-brainer, but you would be surprised how rarely anyone opens it during a rush.
Step 2: Put the job on the right Boss Laser machine
Loading the first machine that is free is tempting. That is how you end up nesting a 30-inch part on a 20-inch bed, or trying to mark bare metal with a CO2 tube. Large sheets belong on the Boss Laser LS-3655 when the layout exceeds the LS-1630 table. Smaller, detailed parts are often faster on the LS-1630 because the head travel is shorter. Bare metal marking belongs on the laser fiber marker, not on a CO2 system. The wrong machine does not just risk quality; it can double the runtime, which is exactly what you do not have.
And while the wavelength question comes up constantly, the phrase 'fiber laser nm' is in a lot of search histories. Here is the short answer: fiber laser marking runs at 1064 nm. CO2 systems run at roughly 10,600 nm. That gap is why the fiber machine marks bare metal and the CO2 machine does not.
Step 3: Check the file for duplicates, scale, and orientation
Before the machine warms up, open the file and check three things: the bounding box size, the orientation, and duplicate paths. I once received a file with two copies of every contour on separate layers. It would have doubled the cutting time, and nobody would have noticed until the run was halfway through. Another file had the design mirrored. I caught it on preview only because I looked.
Hide or delete empty layers, confirm color mapping, and compare the bounding box with the material dimensions. This takes about 60 seconds. It is the cheapest check on this list.
At the Machine (Steps 4-6)
Step 4: Inspect the CO2 optics before the run
This is the step everybody skips, and it is the step that has cost us the most. If the system uses a CO2 laser lens 20mm and mirrors 25mm, a contaminated lens can look like a focus problem while the machine is running. The lens can look clean from the top and still have a faint film on the underside.
The event that changed my rule: In March 2024, we accepted a 36-hour rush order for 120 acrylic displays. The LS-1630 had run fine the previous day, so I skipped the optics check and loaded material. Ninety minutes in, the edges started charring and the laser stopped cutting through. We stopped, pulled the lens, and cleaned residue from a rubber stamp test done the day before. The cleaning took twenty minutes. The lost production, test cuts and re-cutting took three hours. The client got the order, but we had almost no buffer left. The most frustrating part is that I knew better; a deadline just made me rationalize skipping the check.
Now the shop rule is simple: no optics check, no start. That rule applies to rush jobs more than any other.
Step 5: Set focus, then run a test on the actual material
Set the focus using the method in the Boss Laser LS 1630 manual (or the procedure for the machine you are using), then cut a small test shape on the exact material you will run. Not on 'similar' material. Same thickness, and from the same batch if possible.
If you are running the Boss Laser LS-3655 with a full sheet, put the test shape in a corner of that same sheet. That way you test the actual sheet height, not a separate scrap that may sit differently on the honeycomb. If the test result is bad, change one variable at a time: focus first, then power, then speed. Change everything at once, and you will not know what actually fixed it.
Step 6: Confirm air assist, exhaust, and chiller are on
After a busy week, the air compressor can be off, the exhaust hose can be disconnected from a cleaning, or the water chiller can be in standby. On a CO2 laser, missing air assist causes flames and poor cut edges. Missing exhaust deposits smoke residue on the lens, which brings you right back to step 4.
Do the 30-second check: air through the nozzle, airflow at the exhaust vent, chiller temperature in the normal range. If the machine has been idle for more than a day, this is the check that prevents a fire and a dead lens.
Before the Run (Steps 7-8)
Step 7: Run the trace or preview mode first
If the control software has a trace or preview mode, use it to watch the head path before the laser fires. You are looking for two problems: long diagonal jumps that mean a stray vector line, and paths that repeat on the same contour. Both are invisible in a still preview. Seeing the head move over a full sheet takes about 30 seconds and can save the whole run.
Step 8: Set an abort threshold before you start
Decide in advance what 'bad' looks like and how many bad parts you can absorb. For a job of 120 parts at 12 parts per hour, you cannot afford to discover a problem after 90 minutes. So set a stop rule: if the first full part fails, stop the job and reassess before reloading. A short, uncomfortable call beats a missed deadline.
When the Run Starts (Steps 9-10)
Step 9: Stay near the machine for the first ten minutes
Most problems appear early. Watch the first full part complete, listen for the normal hiss of air assist, and check the cut or engraving quality once the head has made a full pass. If something is wrong, you stop in seconds instead of after half a sheet has been ruined. The paperwork can wait ten minutes.
Step 10: Write down the settings that worked
When the job is running cleanly, record the material, thickness, lens focal length, speed, power, air assist pressure, and raster or vector mode. A shared notebook is fine. When the same order comes back in two weeks, that note will save you a test cycle. It also gives you a baseline if the machine slowly drifts out of spec.
The Mistakes That Eat Deadline Jobs
Three mistakes show up again and again:
'It worked yesterday.' Yesterday's material is not today's material, and the lens was not dirty yesterday. The 'it worked' assumption caused my March 2024 failure.
Testing on scrap instead of the actual sheet. Scrap is useful for verifying power. It is not useful for verifying focus at the height of the sheet you are about to cut. Differences in material flatness change the result.
Hiding a bad first test. If the first test shape is wrong, stopping and diagnosing is faster than letting the run continue. The machine will not fix itself at minute 45.
Bottom Line
In rush work, the operator is the bottleneck. The machine will not go faster because the client is waiting. The only real speed available is avoiding rework. A fifteen-minute checklist before hitting start is not a delay; it is the fastest route to done.
Setup references in this guide are based on Boss Laser published documentation and machine spec sheets, checked as of January 2025. Machine generations vary. Verify against the manual for your specific unit.