Short answer up front
If you're spec'ing your first CO2 laser and you're somewhere around Nocatee or Naples, FL, here's the answer straight: the Boss Laser 1630 is a solid choice for most shops running 60W–80W on a 16x30" bed — but the real delivered cost usually runs about 20% above the base quote once you add a chiller, fume extraction, spare optics, and one spare tube. Shops that only budget the machine price get caught off guard by month two.
I've been on the receiving end of 200+ laser machine deliveries a year. Here's what I actually check, and where the 1630 holds up.
Why you can take this seriously
I'm the quality and brand compliance manager at a contract manufacturing shop. Every laser cutter or fiber marking system that lands on our floor passes across my inspection bench before it goes into production. Over four years of reviewing deliveries — CO2, fiber, hybrid — I've put hands on 800+ units. In our Q1 2024 audit, roughly 12% of first-arrival lasers got sent back to suppliers for failed incoming setup or laser calibration drift outside spec.
I'm not bringing that up to scare you. I'm bringing it up because I have a tolerance threshold, and the LS-1630 sits clearly inside it for its class. That's a specific claim, and I'll show you why.
What the 1630 actually is
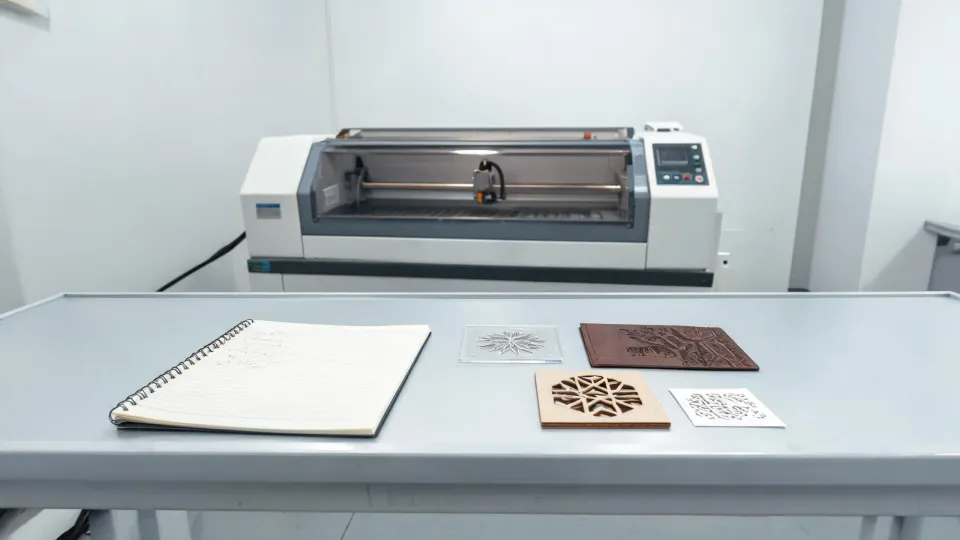
Boss Laser 1630 — the LS-1630 series — is a 16x30" bed, CO2 source, 60W–100W depending on configuration. It's built for what?
- Mid-volume acrylic cutting
- Wood engraving
- Leather marking
- Non-metallic job shop work
It's not built for high-volume production running three shifts. That's a different machine class, and honestly, a different budget.
Here's the counterintuitive part: plenty of first-time buyers walk in wanting to cut stainless steel signage on a 1630. It can sort of do this on very thin stock with assist gas, but "can" and "should" aren't the same thing. Edge yellowing, dross, warping — post-processing eats more time than the cut saved. If metal marking is your actual target, you want a fiber laser setup, not a CO2 machine. Those are two different projects.
The Boss Laser price math nobody tells you
Boss laser price on the spec sheet looks reasonable. That's the machine alone. Here's the real delivered number:
- Machine itself (varies by wattage and options)
- Water chiller — effectively mandatory above 80W
- Fume extraction or filtration — you can't run this thing in an enclosed space without it
- Spare lenses and focus mirrors — don't wait until one burns
- Install/commissioning labor or freight
Add those. That's what you actually pay. If a rep only quoted you the unit, top up the rest yourself before you commit.
One case I still think about: a 43-unit order came in, and roughly three out of ten of the 60W units had edge charring beyond spec. The vendor called it "within industry standard." Our internal standard is char width under 0.2 mm. Theirs ran to 0.5 mm. We rejected the batch, they redid it at their cost, and from then on every contract we write includes char width tolerances. The lesson isn't about any one brand — it's that a written incoming spec beats a verbal promise every time.
Setup matters more than wattage
Everything I read said buy the highest wattage you can afford. In practice, a well-tuned 60W with a clean beam path and proper focus calibration beat a poorly dialed-in 100W every single time.
Say it again for the people in the back — people assume more watts equals better results. What actually happens: a 100W machine with an unaligned tube, dirty optics, and no power-vs-speed curve set for the material cuts worse than the 60W you tuned properly. You paid more and bought more trouble.
Whether you're sourcing a co2 laser Nocatee or a co2 laser Naples fl, buy the service alongside the hardware. Can somebody walk your team through initial beam alignment? Is there remote or onsite setup support? That's worth more than another 20W.
And here's the thing that still frustrates me about this whole industry: the same issues recur even when the spec is written plainly. You'd think a clear spec sheet prevents misunderstanding. It doesn't. Batch consistency comes from suppliers who control their process year over year — not from writing more clauses into the contract.
When paying for certainty actually pays back
Here's the piece that tends to get skipped when people compare quotes: time certainty. A machine $400 cheaper that arrives three weeks late and misses a client's window saved you nothing.
Our rule on the floor is simple. On deadline-critical jobs, we pay a premium for delivery certainty, not speed. Not because we like spending money — because an uncertain cheap option ends up more expensive than a slightly pricier sure thing. A missed deadline costs multiples of any rush fee.
If you're staring down a trade show order or a customer sample drop, don't save $300 on an ambiguous lead time. The savings won't cover one missed commitment.
What I'd do if I were picking one
If you're at the selection stage right now in Florida, here's what I'd actually do:
- Define your materials first. Acrylic and wood are the 1630's lane. If you're serious about thin metal, go fiber, don't force it.
- Ask for a full-line quote. Chiller, extraction, consumables, commissioning included — not just the unit.
- Prefer a channel with local feet on the ground. Even at a higher price. When something breaks, somebody who can be at your bench the next morning beats an overseas helpdesk.
- Plan fume extraction before delivery. It's the most commonly overlooked part, and the one that'll chase you out of your own shop on day one.
One last thing — matched wattage plus a clean optical path will outcut excess wattage plus sloppy setup. Every time. Don't buy watts, buy a tuned machine.