-
The Short Answer: Don't Trust the Preset Table
-
Who's Writing This (And Why You Should Care)
-
Why Preset Settings Fail More Than They Work
-
What I Actually Do Instead
-
Glass Etching: Where Boss Laser Settings Matter Most
-
The Hidden Cost When You Buy a Machine
-
Where Preset Settings Are Actually Fine
-
One More Thing on Transparency
The Short Answer: Don't Trust the Preset Table
Here's the thing I wish someone had told me six years ago: the material settings card that ships with your machine is a suggestion, not a spec. On our first boss-laser CO2 unit, the factory preset for 3mm borosilicate glass etching ran at 45% power and 300mm/s. We ran it. We got cloudy gray frosting instead of the bright white etch our client had approved. Six weeks of rework and a $3,400 credit later, we stopped trusting preset tables for anything customer-facing.
That's the conclusion. Everything below is why I hold it, and where it doesn't apply.
Who's Writing This (And Why You Should Care)
I'm a quality and brand compliance manager at a laser engraving shop in the Midwest. My job is to review every machine setup, material test, and first-article sample before it reaches a customer — roughly 200 test cuts a quarter across CO2 and fiber platforms. I've signed off on maybe 1,200 production runs since 2021. I've also rejected about 30% of first samples in that time, and most of those rejections traced back to settings taken off a preset card or a forum post.
When I say "don't trust the preset table," I'm not being dramatic. I mean I have the rejection logs to prove it.
Why Preset Settings Fail More Than They Work
Machine laser engraving has four variables that all interact: power, speed, focal distance, and air assist. A preset card fixes all four. But it can't account for:
- Tube age. A CO2 tube loses output as it ages. Our 100W tube was measuring 87W at six months. Running the same preset at 87W produces a different result than the test lab's 100W.
- Material variance. Glass from a different supplier, even the same nominal thickness, etches differently. Borosilicate vs. soda-lime is a completely different conversation.
- Humidity and ambient temperature. We run in a shop that swings from 35% to 70% relative humidity through the year. Behavior changes.
Here's where a lot of buyers go wrong: they see "preset = faster startup" and assume the print on the card is a quality-controlled spec. From the outside, it looks like the manufacturer did the hard work for you. The reality is that a preset card is a marketing convenience — a selling point that reads well on a spec sheet, not a manufacturing standard the factory will stand behind when your etch looks wrong.
What I Actually Do Instead
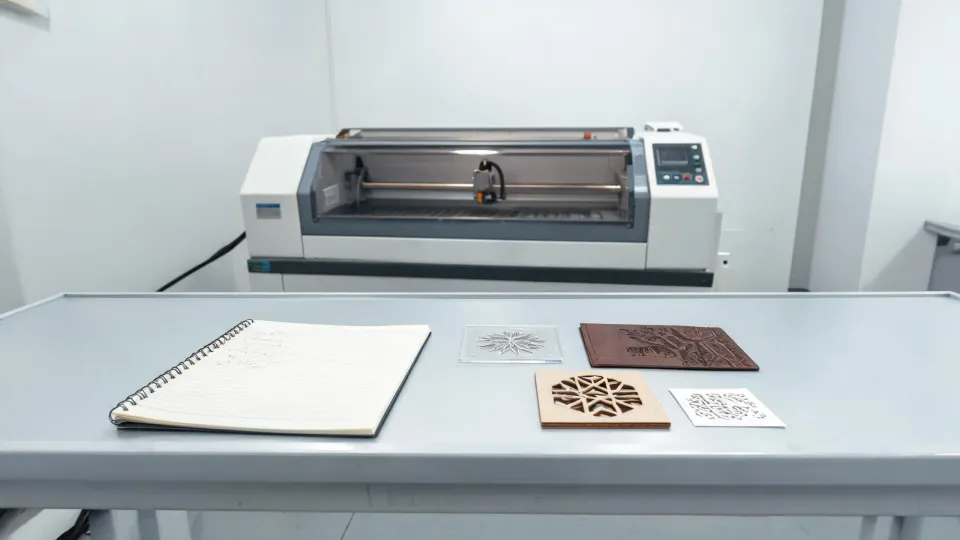
Every new material gets the same treatment: a 5x5 test grid. Five power levels, five speeds, one focal setting, and an air-assist constant. 25 squares, labeled. I keep the grid in a binder with the project date, material batch number, tube hours, and ambient humidity.
When a job comes in, I don't ask "what setting does the machine have?" I ask "what batch is the material from, and what does the binder say?" That process has paid for itself. It's the only boss laser material settings source I trust — the one we built ourselves.
Glass Etching: Where Boss Laser Settings Matter Most
Boss laser glass etching is where the preset table causes the most expensive errors, because glass is unforgiving. Over-power it and you get cracks from thermal stress. Under-power it and the etch is shallow and fades when the customer washes it (which, honestly, they always do). There's a narrow band that works, and it moves with every supplier change.
On our boss-laser glass etching line, we've found that soda-lime drinkware etches cleanly at 28–32% power and 250mm/s with air assist at 30 PSI. Borosilicate needs 35–40% power and drops to 220mm/s. Those numbers aren't from the manual. They came from a rejection we did in October 2023 where a customer sent back 240 etched glasses because the etch was too shallow to be dishwasher-safe.
We never had a formal material-receipt process before that. Cost us when the supplier switched soda-lime to borosilicate without telling us, and we ran the old preset for six production days. We remade the whole order at our cost — about $1,800 in glass and 30 hours of machine time. Saved maybe 20 minutes by trusting the preset. Ended up spending a full reprint. On glass, the preset is the single most expensive shortcut in the shop.
The Hidden Cost When You Buy a Machine
This is where the CO2 laser pricing conversation usually gets lost. Buyers searching "laser co2 precios" or comparing quotes from different CO2 laser marking machine manufacturers often fixate on the headline number. I get it. But the purchase price isn't the cost. The cost is the price plus the time it takes to build a working settings library for your actual materials.
If a vendor hands you a machine and a preset card and says "you're ready," that's a red flag. What you actually want is a vendor who tells you upfront how long calibration takes — typically 15–40 hours of test cuts for a mixed material lineup — and what support looks like when a setting stops working.
When we were evaluating our second machine, I asked every CO2 laser marking machine manufacturer the same question: "What's NOT included in the training?" The answers were revealing. One vendor said "everything's included" — which told me they hadn't thought about it. Another rep talked about tube current documentation, material batch logging, and a setting-library template. That's the answer that actually helps.
The quoted price on a machine is never the full number. The vendor who tells you that upfront — even if the total looks higher on the page — is the one you'll spend less with over three years. I've learned to ask "what's not included" before "what's the price."
Where Preset Settings Are Actually Fine
I should be honest about the limits of my own position. Presets are fine for:
- Non-critical marking on consistent, single-source material (steel tags, anodized aluminum) where a small variance in darkness doesn't matter to the customer.
- First-pass prototyping where you're using the cut to figure out the design, not the finished part.
- Rental or loaner machines where you're not going to invest in a full calibration cycle.
For anything a customer will see, sign off on, or return — do the grid. It's 20 minutes and it prevents the redo. That's the ballpark trade: 20 minutes upfront, or a full remanufacture on the back end.
One More Thing on Transparency
Here's what I'd want a buyer to know: if a machine supplier won't tell you their settings are starting points, that's a small transparency problem. If they won't tell you what training and support cost after purchase, that's a bigger one. Running the arithmetic before you buy — machine cost, tube replacement timeline, calibration hours, and support tier — will tell you more about the real price than any headline number on a quote sheet.
That's not a knock on any specific brand. It's just how the numbers actually add up when you put them in a spreadsheet instead of a sales deck.