-
Three scenarios (and one edge case) that cover most buyers
-
Scenario 1: Multi-material shop → CO2, and don't overthink the wattage
-
Scenario 2: Metal-dominant operation → 200W fiber, but read the fine print
-
Scenario 3: Inline production → flying CO2 marking, but check the math twice
-
The edge case: copper and highly reflective metals
-
How to figure out which scenario you're actually in
When I first got handed our capital equipment budget, I thought picking a laser came down to comparing spec sheets and finding the one with the best numbers. Six years and 41 purchase orders later — roughly $380,000 in cumulative equipment spend — I know that's not how it works.
The question isn't which laser is best. It's which laser fits the work you're actually going to run, at the volume you'll actually run it, with the downtime you can actually absorb. Those three variables change the answer completely.
So instead of giving you one recommendation that'll only be right for a fraction of readers, here's how I'd structure the decision. Find your scenario, read that section, skip the rest.
Three scenarios (and one edge case) that cover most buyers
In my experience, almost every laser purchase I've been involved with falls into one of these:
- Scenario 1: A multi-material shop — wood, acrylic, leather, anodized aluminum, occasional coated metal. Small-batch work.
- Scenario 2: A metal-dominant operation — marking, cutting or welding steel, stainless, aluminum. Throughput matters.
- Scenario 3: Inline production marking — date codes, lot numbers, traceability marks on moving product.
Then there's the one nobody brings up in the sales call: copper and other highly reflective metals. That gets its own section because the rules are just different.
Scenario 1: Multi-material shop → CO2, and don't overthink the wattage
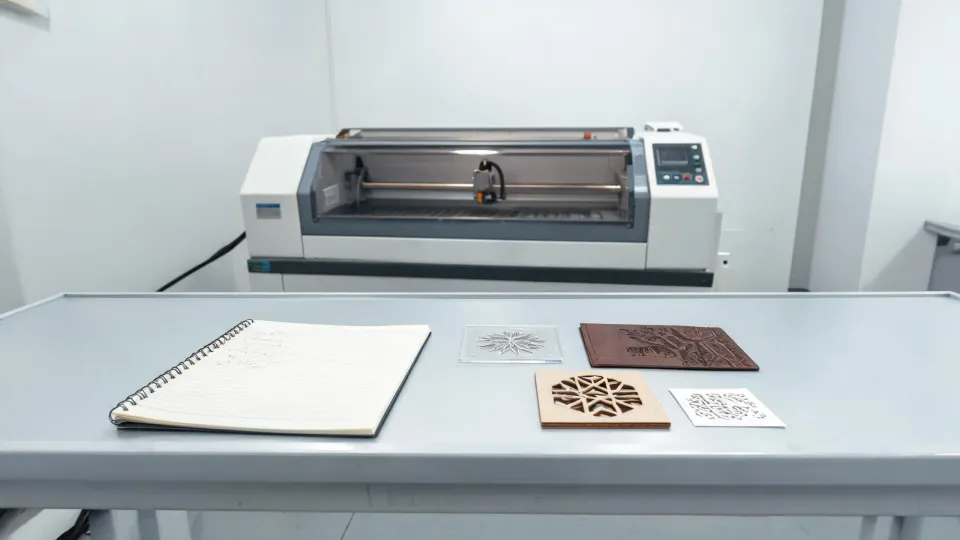
If your job board looks like mine did in 2022 — half acrylic signage, a quarter leather goods, some plywood prototypes — you want a CO2 platform. Full stop. Fiber lasers don't cut organics well, and diode lasers are a different discussion entirely.
A machine like the Boss LS-1630 or the smaller LS-1420 covers this ground pretty thoroughly. Here's what I'd flag from a cost perspective, though:
The purchase price is roughly 60% of your first-year cost. I'm not exaggerating. When we brought in our first CO2 unit back in Q2 2022, the quoted machine price was $9,400. By the end of year one, we'd spent an additional $5,800 on:
- Chiller and ventilation setup: $1,900
- Two lens replacements (we cracked one, wore out the other): $740
- Waste from parameter tuning — roughly 30 hours of material we couldn't sell: $2,100
- Spare mirrors and alignment tools: $380
- An unplanned belt replacement: $680
That last one still irritates me. The belt failed at month nine and the vendor's 'warranty' excluded wear items. Read your warranty exclusions before you sign — not after.
One thing people underestimate: material settings. A solid parameter library saves you weeks. Boss publishes a starter set and their user community fills in the gaps, but even then, expect 15–25 hours of scrap material before you dial in your specific stock. Budget for it. Don't pretend it won't happen.
People think a more expensive machine cuts better. It's closer to the reverse — machines that consistently cut better end up commanding higher prices. The causation runs the wrong way in most buyers' heads.
Scenario 2: Metal-dominant operation → 200W fiber, but read the fine print
If your jobs are 70%+ metal, CO2 is the wrong tool. Fiber is the answer, and for most small-to-mid shops, 200W fiber hits the sweet spot.
Here's where I'd push back on the usual advice. Every vendor I've talked to wants to upsell wattage. 500W, 1kW, 1.5kW. And for a minority of buyers that's correct. For most, it's a waste of capital.
The misconception: higher wattage means lower per-part cost.
The reality: higher wattage means higher electricity draw, higher cooling load, more expensive consumables, and a bigger service contract. If you're running thin sheet and small parts, those extra watts sit idle 80% of the time while you keep paying for their upkeep.
What I'd actually check instead:
- Laser source brand. Raycus vs. IPG vs. Max is a real cost difference — sometimes $2,000–$4,000 on the same frame. It also impacts resale value.
- Rated duty cycle at your real workload. Not the marketing number. Ask for the thermal test data.
- Service response time in writing. 'Same-day support' means nothing without a written SLA.
Rough pricing as of December 2024, from quotes we collected across six suppliers: a bare 200W fiber marking platform ran $6,800–$18,500 depending on source brand and work envelope. Add a chiller ($600–$1,200), rotary axis if needed ($400–$900), and fume extraction ($500–$1,500). Real out-the-door is closer to $8,300–$22,000.
I still kick myself for not getting our first fiber vendor's verbal delivery commitment in writing. They promised 3 weeks, delivered in 9, and we'd booked jobs against that timeline. Cost us about $4,100 in outsourced work we could've done in-house.
Scenario 3: Inline production → flying CO2 marking, but check the math twice
If you're marking product on a moving conveyor — date codes, batch numbers, barcodes for traceability — you're looking at a flying CO2 laser marking machine, not a flatbed. Different animal, different economics.
The frustrating part: vendors quote these as if you're buying a standalone system. You're not. You're buying an integration project.
What nobody told me before our first inline rollout:
- Conveyor speed matching isn't plug-and-play. Expect 20–40 engineering hours to sync the laser with your line.
- You need a mounting solution specific to your line frame — usually $600–$2,000 custom fabricated.
- Safety interlocks and enclosure requirements vary by jurisdiction. Check your local regs before you spec the machine.
- Downtime during install is real. We lost 3 production days. That's roughly $6,300 in output for our line.
A flying CO2 system from a reputable supplier lands somewhere between $12,000 and $28,000 depending on power, marking field, and software. But the true installed cost is usually 30–50% higher than the quote. Plan accordingly.
The edge case: copper and highly reflective metals
Now the one that trips up a lot of buyers — fiber laser copper processing.
Short version: yes, a 200W fiber can mark copper. No, it won't cut it well. And no, more wattage doesn't usually fix the problem.
Here's the physics in plain terms. Copper reflects around 95% of the 1064nm wavelength that standard fiber lasers emit. You're dumping power into a mirror. Some of it gets absorbed once the surface heats up, but you're fighting an uphill battle the whole way.
The assumption is that copper is hard to cut because it's dense. The reality is it's hard because it's reflective — at the specific wavelength your laser uses. Different wavelength, different story.
What actually works for copper:
- Green (532nm) or blue (450nm) lasers — dramatically better absorption. Also dramatically more expensive.
- High-peak-power pulsed fiber — can mark, rarely cuts cleanly at production speeds.
- Outsourcing — if copper is under 10% of your workload, this is almost always cheaper than buying a second machine.
If a supplier tells you their standard 200W fiber will 'handle copper no problem,' ask them for sample parts and a cycle time. That conversation usually ends pretty quickly.
How to figure out which scenario you're actually in
Answer these honestly. Not aspirationally — actually.
- What percentage of your jobs are non-metal? Above 40% → lean CO2. Below 15% → lean fiber. In between → you probably need both, or need to pick the dominant one and outsource the rest.
- What's your monthly throughput at peak? Under 200 hours/month → don't buy industrial. 200–600 hours → mid-tier. Above 600 → industrial platform, and service contracts matter more than sticker price.
- Is the laser going into a production line or a standalone cell? Inline → add 30–50% to the quote for integration and downtime. Standalone → quote plus 15% for setup.
- Do you have service nearby? If the nearest technician is 8 hours away, factor in the downtime cost of every service call. Sometimes the cheaper machine becomes the more expensive one.
And one more thing — on the timing question. Every year around Boss Laser Black Friday season, I get asked whether to buy now or wait. Here's my honest take: promotional pricing is real, but so is the pile of buyers who rush a decision because a discount expires. If you've done your TCO homework, a sale is a nice bonus. If you haven't, a sale is just a faster way to make an expensive mistake.
Do the math first. Then look at the calendar.